What Are the Top Types of Reaction Injection Molding?
Reaction Injection Molding (RIM) is often described as one process, but manufacturers use several important variations. The differences are practical. They affect stiffness, weight, surface feel, and how a part performs under impact. A vehicle fascia, a cushioned equipment cover, and a reinforced industrial panel do not need the same material recipe.
Otto Bayer, whose polyurethane research helped lay the foundation for RIM, offers a useful historical perspective. The following is a paraphrase, not a verified verbatim quotation: “Control the chemistry, and the process becomes more predictable.” That principle still matters. In RIM, liquid components are metered, mixed, and injected into a closed mold, where they react and form a solid part. Small changes in temperature, mixing, or mold design can affect the result. The process is precise, but not effortless.
This guide examines the top types of Reaction Injection Molding, including standard polyurethane RIM, reinforced RIM, and structural RIM. Each serves a different purpose. Reinforcement can improve rigidity, while unreinforced formulations may suit lighter or more flexible components. Names and classifications sometimes overlap across suppliers, so product labels alone can be misleading. That deserves a closer look. The right choice depends on the part’s geometry, load, finish, production volume, and operating environment—not simply on which process sounds most advanced.
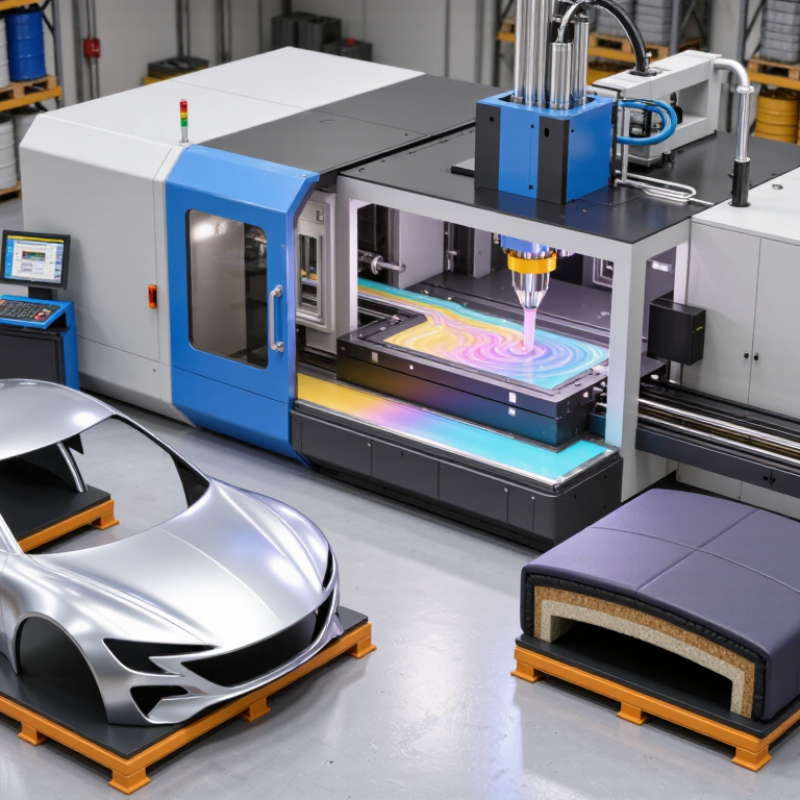
Classify RIM by Resin, Reinforcement, and Cellular Structure
What Are the Top Types of Reaction Injection Molding?
Reaction injection molding is best classified by resin, reinforcement, and cellular structure. Polyurethane RIM is common for large, lightweight housings and panels. Polyurea systems can offer flexibility and impact resistance, while other reactive resins serve specialized needs. Performance depends on formulation, mold temperature, and cure conditions. That detail is easy to overlook.
By reinforcement, standard RIM uses unfilled resin, while reinforced RIM, or RRIM, adds short fibers or mineral fillers for stiffness and dimensional stability. Structural RIM places a continuous fabric or fiber preform inside the mold. It can produce stronger, load-bearing parts, but preform placement takes care. Parts may also be solid or cellular: integral-skin foam has a dense outer layer and a lighter core. These categories can overlap.
Tips: Match the process to the part’s job. For a broad panel, compare weight, stiffness, and surface finish. Check wall thickness and vent locations with a molding specialist; small geometry changes can affect filling and curing. It is not always obvious which trade-off matters most.
Conventional Polyurethane RIM: Typical Injection Pressures Are About 0.7–1.4 MPa
Conventional polyurethane reaction injection molding (RIM) uses relatively low injection pressure compared with many thermoplastic processes. A typical range is about 0.7–1.4 MPa, or roughly 100–200 psi. Technical references such as Günter Oertel’s Polyurethane Handbook describe RIM as a reactive, low-pressure molding process. The figures are a practical reference, not a universal setting. Actual pressure depends on the mixhead, material formulation, flow path, and measurement location.
That distinction matters. A pressure reading at the machine may not match pressure inside the mold cavity. Operators assess the process alongside shot size, component temperature, and fill time. For example, a long, thin rib may need a different setup than a broad, shallow panel. The pressure range alone cannot predict whether the cavity will fill cleanly. Keep records from each trial. Small changes can shift the result. A pressure that works on one tool may cause incomplete filling or excess flash on another. Technical guidance, including Szycher’s Handbook of Polyurethanes, supports treating process conditions as application-specific. The range is useful, but it deserves verification on the actual machine.
Conventional Polyurethane RIM: Typical Injection Pressure
Typical injection pressure is about 0.7–1.4 MPa. The midpoint shown is calculated from the two ends of this range.
RRIM: Chopped-Glass Reinforcement Commonly Uses Fibers Around 6 mm Long
In reaction injection molding, RRIM adds chopped glass fibers to a reactive resin before the material enters the mold. Fiber lengths around 6 mm are common. They can improve stiffness and help molded parts resist bending, especially in broad panels and structural housings. The exact result depends on resin chemistry, fiber loading, mold design, and processing conditions.
Six millimeters is a useful reference, not a guarantee. Fibers may shorten during mixing and injection, while their direction can vary across a part. A ribbed corner may therefore behave differently from a flat section. Good dispersion matters: clumps can create weak spots, rough surfaces, or uneven appearance. More reinforcement is not always better. It may also affect flow and surface finish.
Tips: Check the supplier’s stated fiber length and loading, then test a representative molded sample. Look closely at corners, thin walls, and attachment points. Ask how processing affects the final fiber distribution. Small differences matter. A sample test cannot replace production validation, but it can reveal problems early.
SRIM: Compare Reinforced-Part Tensile Strength Using ASTM D638
Structural reaction injection molding (SRIM) places a reinforcement mat in the mold before resin injection. That changes the comparison. A glass mat can carry load along its fibers, while the polyurethane matrix transfers stress between them. ASTM D638-22 provides a consistent tensile-test method, but it does not set one universal SRIM strength value. Results depend on fiber content, orientation, thickness, and specimen preparation.
For a useful comparison, test reinforced and unreinforced parts under the same conditions. ASTM D638 Type I specimens have a 13 mm narrow-section width and a 50 mm gauge length; record the specimen thickness too. Calculate tensile strength from the maximum force divided by the original cross-sectional area, then report individual results and the average. Small details matter. A cut edge with exposed fibers can become the point where a specimen breaks, masking the material’s broader performance. Note the break location and fiber direction alongside each result. It is tempting to rank SRIM parts by one headline number. That number can mislead when test setup or reinforcement alignment differs. Cite ASTM D638-22 with the data so readers can judge whether the comparison is fair.
Microcellular RIM: Measure Foam Density in kg/m³ Using ASTM D1622
Microcellular reaction injection molding creates lightweight parts with fine gas cells distributed through a polymer matrix. Foam density, reported in kg/m³, helps engineers compare batches and assess whether a component meets its design needs. ASTM D1622 provides a method for determining the apparent density of rigid cellular plastics. The basic idea is simple: measure a specimen’s mass and volume, then calculate density. Simple, but not foolproof.
Prepare and measure specimens according to the current standard, using suitable equipment and documented conditions. A small sample can be weighed on a calibrated balance, while its dimensions help establish volume. For irregular shapes, use a suitable volume-measurement method allowed by the standard. Keep the specimen dry and note whether its molded surface skin remains; skin and cut edges may affect results. Report the method, specimen details, and density in kg/m³. Repeat measurements across several locations or parts when practical. Variation can reveal uneven cell structure or process drift. Density alone cannot describe every foam property. It will not show cell size or strength. That limitation matters. Results also depend on careful sampling, and inconsistent cuts can weaken an otherwise sound comparison.
What Are the Top Types of Reaction Injection Molding? — Microcellular RIM: Measure Foam Density in kg/m³ Using ASTM D1622 | Specimen | RIM Material | Length (mm) | Width (mm) | Thickness (mm) | Volume (m³) | Mass (g) | Apparent Density (kg/m³) |
| MRIM-01 | Microcellular polyurethane | 100 | 100 | 25 | 0.000250 | 80.0 | 320 |
| MRIM-02 | Microcellular polyurethane | 100 | 100 | 25 | 0.000250 | 90.0 | 360 |
| MRIM-03 | Microcellular polyurethane | 100 | 100 | 25 | 0.000250 | 100.0 | 400 |
| MRIM-04 | Microcellular polyurethane | 100 | 100 | 25 | 0.000250 | 110.0 | 440 |
| MRIM-05 | Microcellular polyurethane | 100 | 100 | 25 | 0.000250 | 120.0 | 480 |
| Mean apparent density for this example dataset | 400 kg/m³ |
Example calculation dataset, not certified laboratory results or specification limits. Apparent density is calculated as specimen mass divided by specimen volume; ASTM D1622 covers the apparent density of rigid cellular plastics. For the listed specimens, 80.0 g ÷ 0.000250 m³ = 320 kg/m³.